Applications of Water Soluble Film Packaging Machines in Modern Manufacturing
Modern manufacturing increasingly relies on packaging systems that can deliver consistent portions, efficient handling, and convenient product formats. Water-soluble film is used in applications where a pre-measured package can dissolve when exposed to water, helping simplify product handling and reduce direct contact with concentrated formulations.
A Water Soluble Film Packaging Machine automates key stages such as film forming, product dosing, pouch sealing, and package handling. POLYVA is one manufacturer providing equipment for water-soluble film packaging applications across different product categories.
Household Cleaning Products
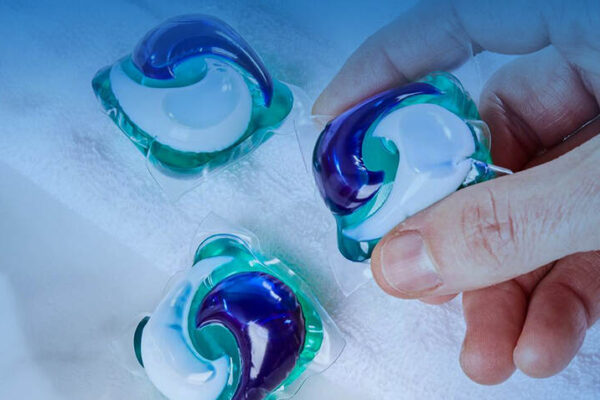
One of the established applications for water-soluble film packaging is household cleaning products. Concentrated detergents, cleaners, and other formulations can be packaged into pre-measured pouches for convenient use.
Single-dose packaging can reduce the need for consumers to measure liquid or powdered products manually. The appropriate film and package design depend on the formulation and intended method of use.
Laundry Products
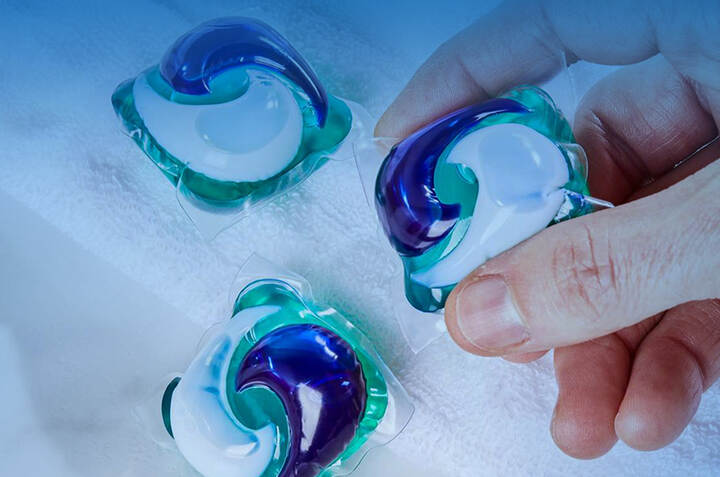
Laundry products are another common application. Detergent formulations can be packaged into individual doses, helping provide consistent quantities for each washing cycle.
Packaging machines used for these products need to provide accurate filling and reliable sealing. Powder and liquid detergents may require different dosing systems because their flow characteristics differ.
Agricultural Products
Water-soluble film packaging can also be used for certain agricultural formulations, including products supplied in concentrated or measured doses. Individual pouches can help simplify handling and reduce the need to manually measure formulations.
Because agricultural chemicals can have specific handling and regulatory requirements, packaging materials and equipment must be selected according to the characteristics and applicable requirements of the product.
Industrial Cleaning Applications
Industrial facilities often use concentrated cleaning and treatment products that require controlled dosing. Water-soluble pouches can provide a measured format that integrates with established cleaning procedures.
Packaging equipment for these applications needs to accommodate the product’s physical properties while maintaining consistent pouch quality during production.
Water Treatment Products
Some water-treatment formulations can be packaged in water-soluble film to provide predetermined quantities. This approach can be useful where accurate dosing is important during treatment processes.
The packaging system must be compatible with the formulation and intended dissolution conditions. Appropriate testing is important to verify package performance before large-scale production.
Construction and Chemical Applications
Certain construction-related and chemical formulations may also use water-soluble packaging where controlled dosing and reduced direct handling are desirable.
The suitability of this format depends on factors such as chemical compatibility, concentration, moisture sensitivity, and the required dissolution behavior. Manufacturers should assess these characteristics before selecting film and packaging equipment.
Hospitality and Commercial Services
Commercial cleaning operations in hotels, offices, healthcare facilities, and other institutions may use pre-measured cleaning products to simplify routine tasks.
Single-dose formats can help standardize quantities across different users and reduce the need for on-site measuring. Packaging requirements vary depending on the product and application environment.
Benefits Across Manufacturing Applications
Although applications vary, water-soluble film packaging can provide several process-related advantages:
- Consistent pre-measured product quantities
- Reduced manual measuring
- Convenient single-dose formats
- Less direct handling of concentrated formulations
- Automated high-volume packaging
- Flexible pouch and compartment configurations
The practical benefits depend on the product, film type, packaging design, and end-use requirements.
Matching Machines to Different Products
Different manufacturing applications require different machine configurations. Liquid products may require controlled pumping and filling systems, while powders can require specialized dosing mechanisms.
Gels and viscous formulations may require additional control during filling. Multi-compartment pouches can also require separate dosing and forming processes to keep different products apart.
Importance of Film Selection
The packaging film is an important part of the overall system. Factors such as dissolution rate, thickness, moisture sensitivity, strength, and compatibility with the product can affect performance.
Manufacturers should test the selected film with the intended formulation and machine settings. Environmental conditions during storage and production should also be controlled according to the film’s requirements.
Role of Automation in Modern Manufacturing
Automated equipment can coordinate film feeding, forming, dosing, sealing, and quality monitoring. This reduces repetitive manual work and can improve consistency across large production runs.
Control systems may also allow operators to monitor machine status, adjust production parameters, and respond to alarms without manually controlling every packaging stage.
Quality and Production Considerations
Before introducing water-soluble packaging into a manufacturing process, companies should evaluate pouch integrity, filling accuracy, dissolution behavior, and compatibility with the product.
Production teams should also consider machine capacity, changeover requirements, environmental controls, maintenance access, and quality-control procedures. These factors influence whether a packaging system can operate reliably at the required production volume.
Conclusion
Water-soluble film packaging machines have applications across household cleaning, laundry, agriculture, industrial cleaning, water treatment, and selected chemical and commercial uses. Their ability to automate measured pouch production makes them suitable for manufacturing environments where consistency and controlled handling are important.
Successful implementation depends on selecting the appropriate film, machine configuration, dosing method, and package format for each product. Careful compatibility testing and process control can help manufacturers achieve reliable packaging performance while adapting the technology to modern production requirements.